

- HOME
- UV PAPER IMPRESSION
- UV PAPER PRODUCTS
- UV PAPER PROCESS
- UV PAPER BLOG
- UV PAPER CULTURE
- UV PAPER TALENTS
Modern deinked pulp (DIP) is bright, strong enough for printing grades and widely used inside coated papers, yet five persistent myths still steer buyers away from specifying recycled content. Those myths describe 1990s technology. This article corrects them with what the process actually delivers today.
This was true when deinking was a two-stage wash process that removed ink but not the fines and sticky residues that dulled the sheet. Modern deinking combines flotation, washing and dispersion stages with enzyme and surfactant chemistry, and the result is a clean, bright furnish.
Commercially, DIP is routinely produced at brightness levels compatible with printing and publishing grades. Recycled content also does not cap brightness at a fixed ceiling: furnish blending, filler selection and optical brightening agents are all engineered per grade. What is true is that very high brightness targets, above the low-90s ISO range, push furnish design toward virgin fibre, because each recycling round shortens and yellows fibres slightly.
Recycling does not destroy fibre, but it does change it. Each cycle shortens fibres and reduces bonding potential, so 100 percent post-consumer furnish will not match virgin kraft in tensile strength. Real-world specifications rarely demand either extreme.
Mill practice blends recycled and virgin fibre to hit strength targets, and reinforcement with long-fibre kraft, refined recycled fibre or strength additives recovers most of the gap. Cast coated and coated woodfree grades use recycled furnish in the base sheet precisely because the coating layer carries the surface performance, while the base is engineered for stiffness and dimensional stability.
Coated papers routinely do. The base sheet is where recycled content lives, with the coating layer, typically clay, calcium carbonate and binders, applied on top. Because print performance is a surface property, the recycled share of the furnish is largely invisible to the press.
The constraint is not technical feasibility but specification discipline: if a grade is designed around recycled furnish, mill systems must keep certified and uncertified streams segregated through chain-of-custody documentation. That is a planning requirement, not a process barrier.
Deinking is water- and energy-intensive, but the comparison that matters is per tonne of finished paper, including the forestry, pulping and transport burden of virgin fibre. Modern mills close water loops with internal treatment and recirculation, and the avoided burden of harvesting, cooking and bleaching virgin pulp is substantial.
Wastewater from deinking is treated to discharge standards, and the residual sludge is increasingly directed to energy recovery. Life-cycle assessments consistently show recycled furnish with a lower environmental burden than virgin across most impact categories, which is why retailer and regulator frameworks credit recycled content at all.
This one is partly true, and the nuance matters. Food-contact legislation in most markets restricts recovered fibre in direct food-contact layers because of migration risk from contaminants that recycling can introduce. So recycled content belongs in outer packaging, non-contact layers and general commercial printing, not the inside face of a food wrapper.
What the myth gets wrong is the scope: restrictions apply to food-contact layers specifically, not to recycled paper generally. Stationery, labels on non-food products, cartons for non-food goods and general print are all unaffected.
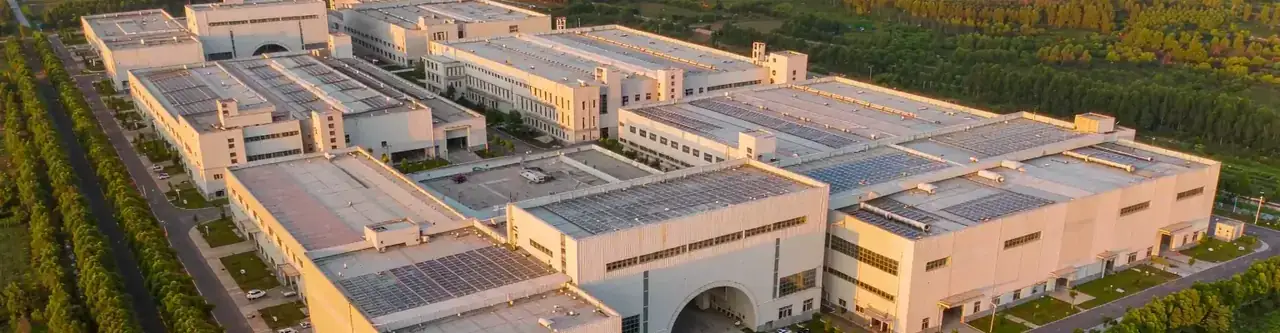
China UV Paper processes 128,000 tonnes of recovered paper per year within a 1.56 million tonne capacity, blending recycled and virgin furnish to hit grade targets on brightness, strength and surface performance. If you are considering a recycled-content specification, our team can confirm what is feasible for your grade and application before you commit artwork.